
Profile-matched tooling
Roll tooling, guides and supports are engineered from the approved cross-section and material grade.
Flexible C and Z purlin production for industrial buildings, warehouses and structural steel projects. The final tooling, layout and guaranteed output are confirmed after we review your profile drawing and production target.
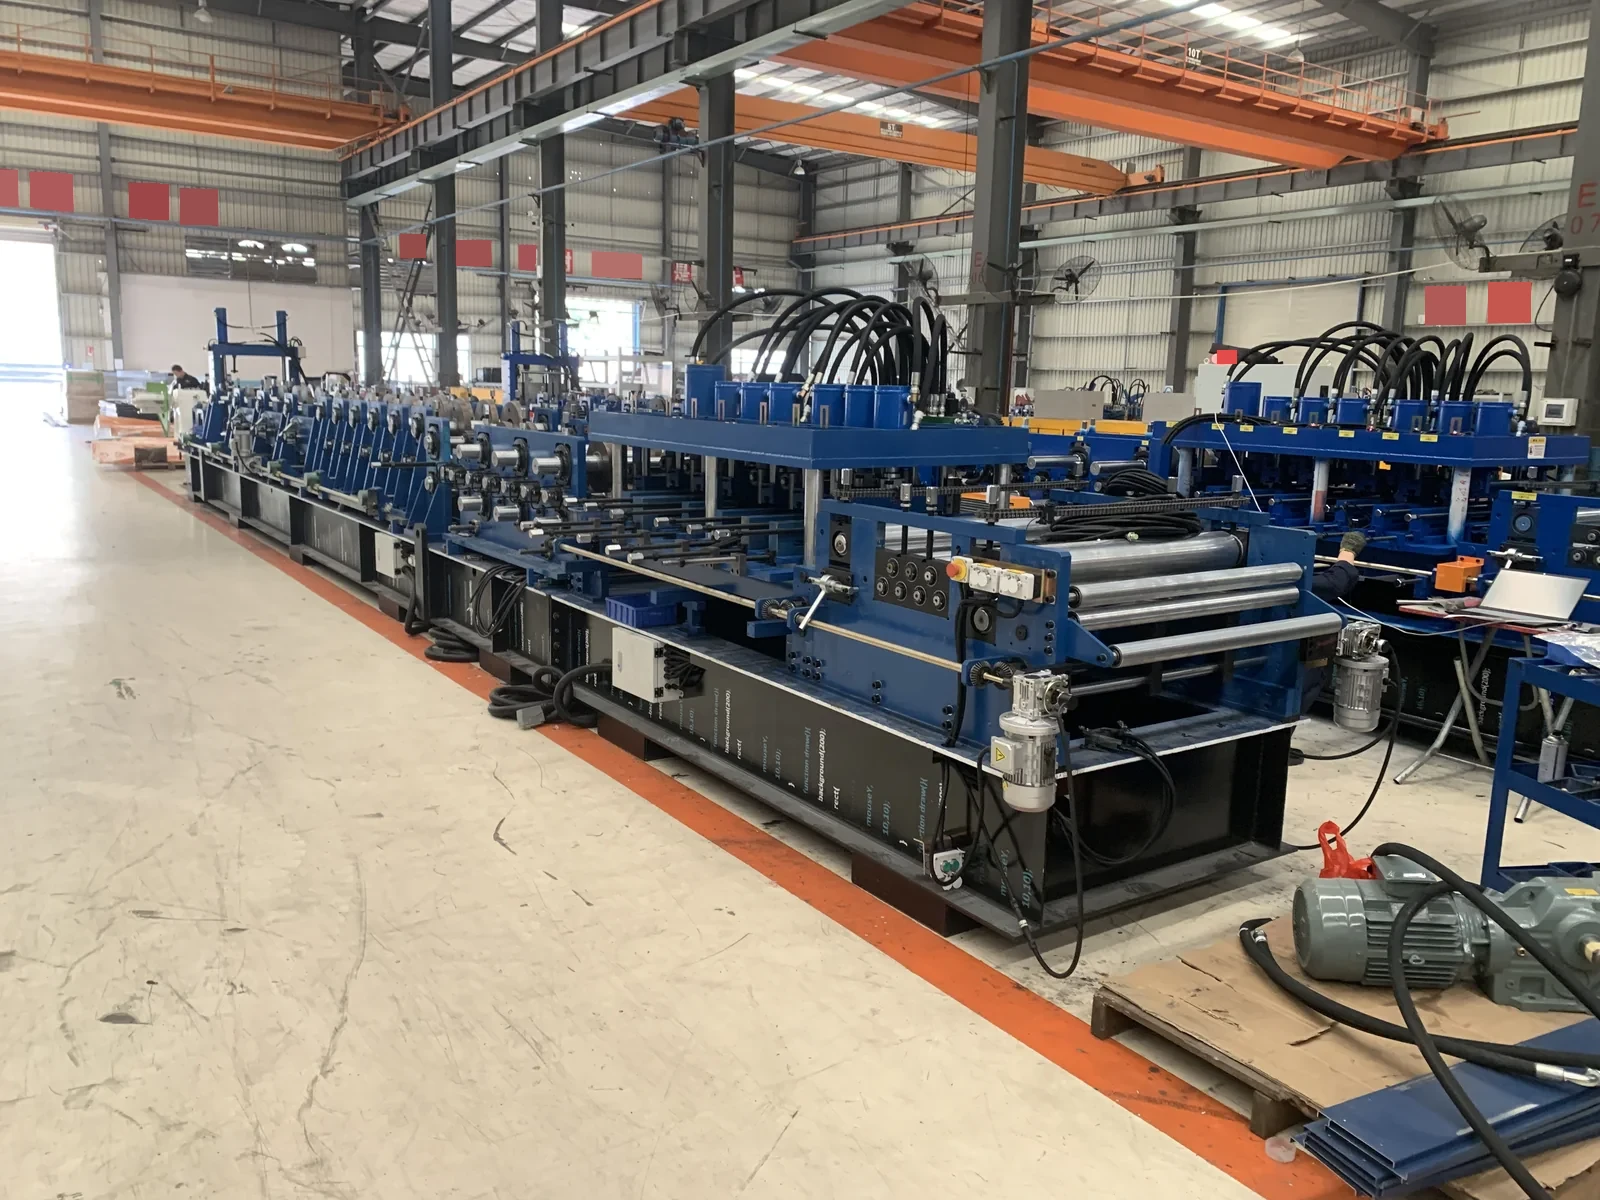
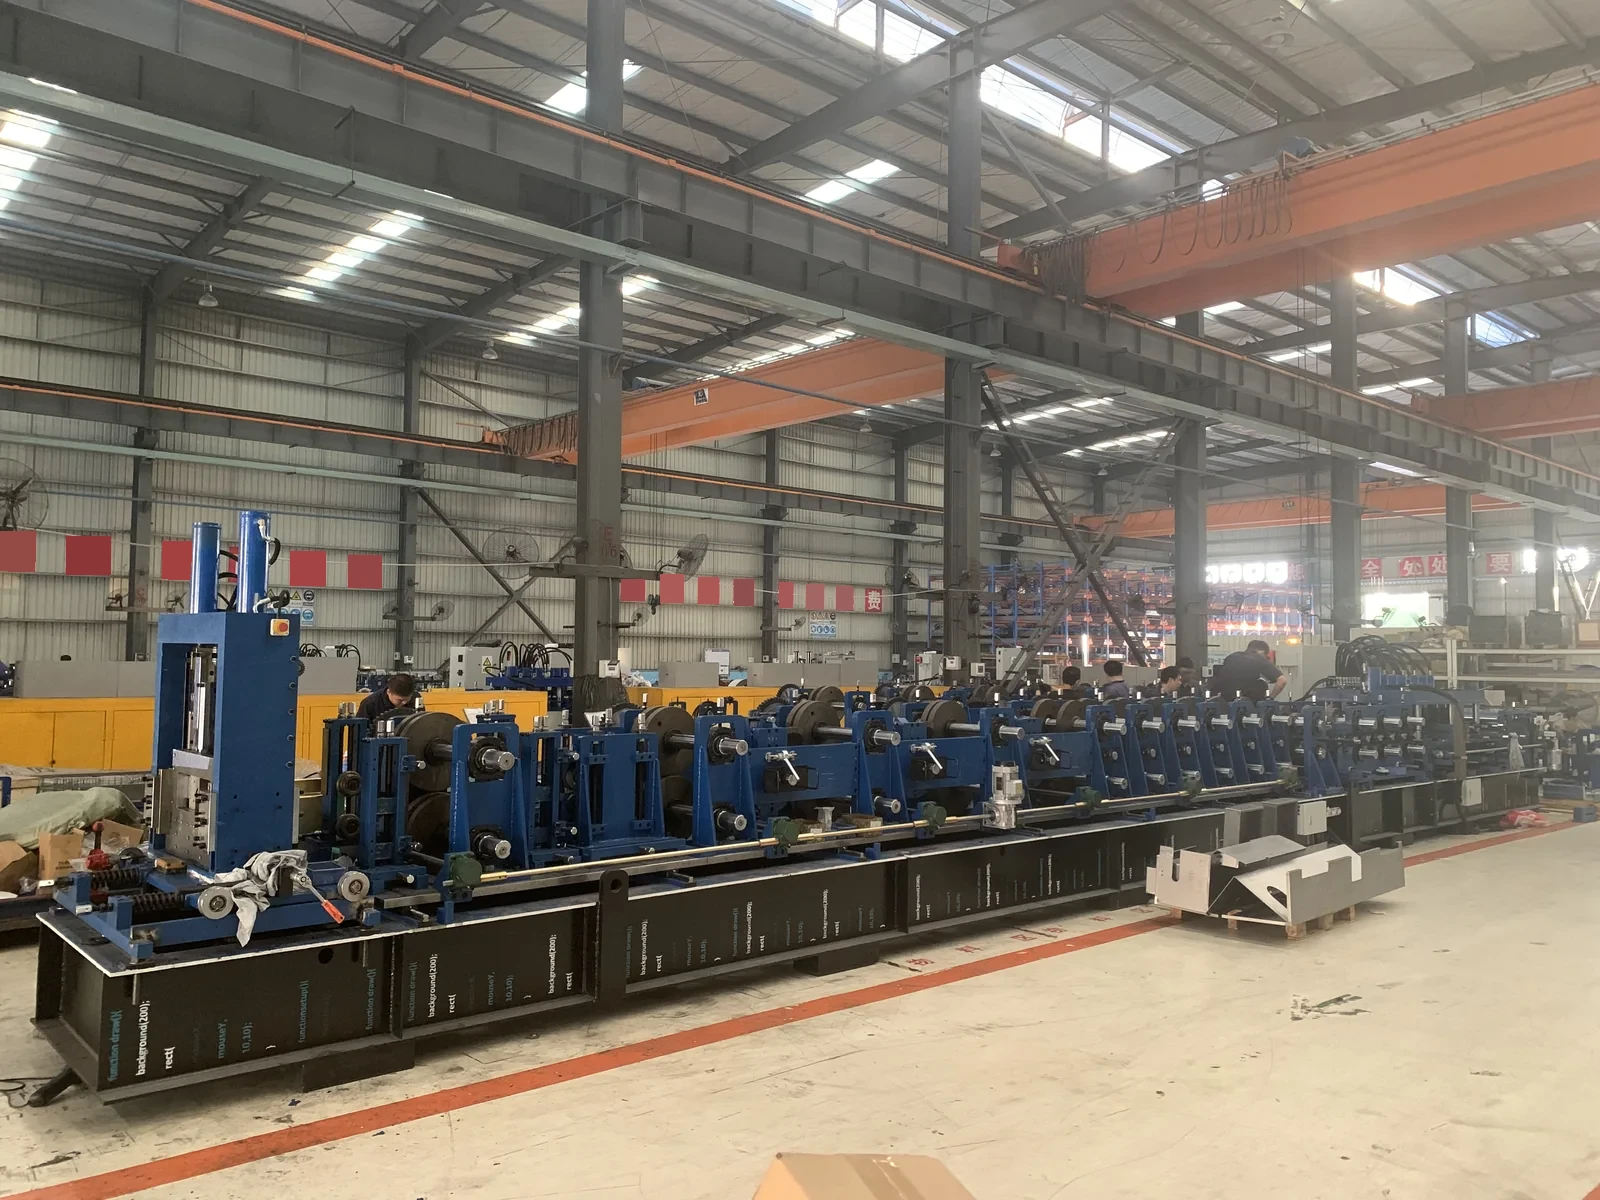
Factory reference image. The comparison below covers separate configurations, not one machine with every listed capability.
Quick answerThe Halcyon automatic C/Z purlin roll forming machine forms C and Z purlins for steel-building roofs and walls from galvanised or black steel coil. Configurations include HCZ-S20, HCZ-300L, HCZ-350A and HCZ-400A, built to your profile drawing. Lead time: 30–60 days for standard machines, 60–120 days for automatic lines, FOB Xiamen, China. Manufactured in our Xiamen factory · 35+ years.
US$39,000–62,000 (standard) · US$72,000–143,000 (premium), FOB China
Standard covers the first two configuration levels (single-profile and multi-profile / quick-change); premium covers fully automatic lines.
Final price depends on profile, thickness, speed, punching and automation. Excludes freight, import duties and installation. Send your profile drawing for a quotation within 24 hours. North American configurations (480V/60Hz, UL and local requirements) are quoted separately.
Large complete lines (e.g. truck chassis beam lines or full cable tray lines) are quoted per project, typically above US$150,000.
Manufactured in our Xiamen factory · 35+ years of roll forming experience.
| Models on this page | HCZ-S20, HCZ-300L, HCZ-350A, HCZ-400A |
|---|---|
| Lead time | standard machines 30–60 days; automatic and heavy-duty lines 60–120 days (confirmed in the quotation). |
| Warranty | 12 months on the machine, lifetime technical support by video and remote guidance; wear parts excluded. |
| Payment | 30% deposit; 70% before shipment, after you approve the trial-run video. |
| Where it is made | Manufactured in our Xiamen factory · 35+ years of roll forming experience. |
| How to get a quote | Send your profile drawing or a photo; we reply with the configuration and price within 24 hours. |
Illustrative sections. Your machine is configured to your own profile drawing.
 Factory photo
 Factory photo
 Factory photo
Send your profile drawing or a photo of the profile. We reply within 24 hours with a configuration and price.
A CZ purlin machine, also called a Cee and Zee purlin roll former, is a C/Z forming line selected for the buyer's approved C and Z sections. Neither name establishes the supplied tooling or verifies the changeover cycle. For a US, Australian or European installation, give the same dimensioned C and Z drawings in clearly stated units, plus steel grade, thickness range, punching layout, target output and the destination power supply. Our factory engineers in Xiamen confirm in the written quotation which profiles and electrical configuration the quoted line supports.
If the decision hinges on a Z-section lap rather than the full C/Z model range, use the Z purlin lap and hole trial checklist to define the sample evidence first.
The engineering starts from the part, material, tolerances, operations, production data and required output.
Roll tooling, guides and supports are engineered from the approved cross-section and material grade.
Punching, marking, cutting and discharge are arranged around the required production sequence.
PLC recipes manage profile size, hole pattern, finished length and batch quantity.
Specify the test coil, sample drawings and measurements needed before shipment; request the resulting records for the quoted configuration.
Compare four configurations by section dimensions, steel grade, thickness and hole pattern. Review each model separately; the largest values in this comparison cannot be combined into a single specification.
Reference-data rule: a range across several machines does not mean every width, thickness and steel grade can be combined. The drawing and coil specification decide the final machine.
The comparison below summarizes the supplied technical specifications for each named configuration. The high-speed figure is the forming-line reference; production with punching depends on hole quantity and spacing.
| Configuration | C / Z web range | Thickness | Reference speed | Main drive | Best fit |
|---|---|---|---|---|---|
| HCZ-S20-300 | C/U 75-300 mm Z 120-300 mm | 1.0-3.0 mm | 30 m/min high-speed forming Punched output: confirm by hole layout | 22 kW | Standard automatic C/Z production, with up to three punching rows in the documented configuration. |
| HCZ-300L | C 80-300 mm Z 120-300 mm | 1.0-3.0 mm | 32 m/min high speed 12-18 m/min typical with punching | Servo drive | Q195, Q235 and Q355B purlins with automatic size change. |
| HCZ-350A | C 80-350 mm Z 120-350 mm | 1.0-3.5 mm | 36 m/min high-speed forming Punched output: confirm by hole layout | 42 kW servo | Wider and heavier purlins, with production-data integration options. |
| HCZ-400A | C/U 100-400 mm Z 120-400 mm | 1.5-4.0 mm | 36 m/min high-speed forming Punched output: confirm by hole layout | 52 kW servo | Wide-flange heavy-duty C/Z work up to a 125 mm flange, subject to profile review. |
Specification source and scope: The C/Z model-family comparison and HCZ-300L technical sheet supplied by our Xiamen production base, reviewed 28 September 2026. The family comparison quotes 15–22 m/min as a combined-speed planning range for all four models; the separate HCZ-300L sheet quotes 12–18 m/min depending on punching quantity. These are different document-level estimates, not measured results for the buyer's drawing. Punched production speed for HCZ-S20-300, HCZ-350A and HCZ-400A therefore remains to be confirmed against the proposed hole layout and acceptance test.
Selection rule: steel grade, flange and lip dimensions, punch pattern and finished length must be reviewed together. Final output, power, accuracy and tooling are confirmed in the signed technical agreement.
If the proposed C/Z line includes holes or slots, compare where the punching station sits relative to forming and how finished parts are measured. Our pre-punching versus post-punching trial guide lists the drawing, feed, die-access and repeat-sample checks; it does not substitute for a quoted station layout.
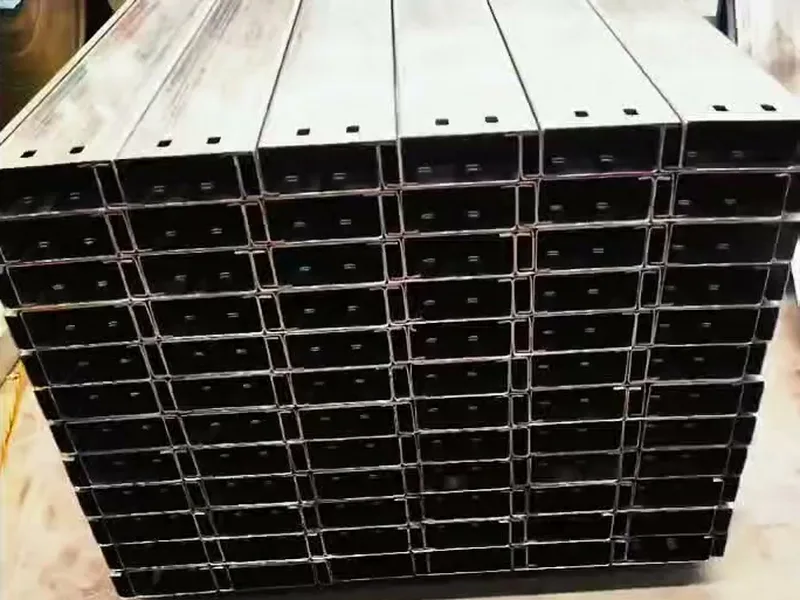
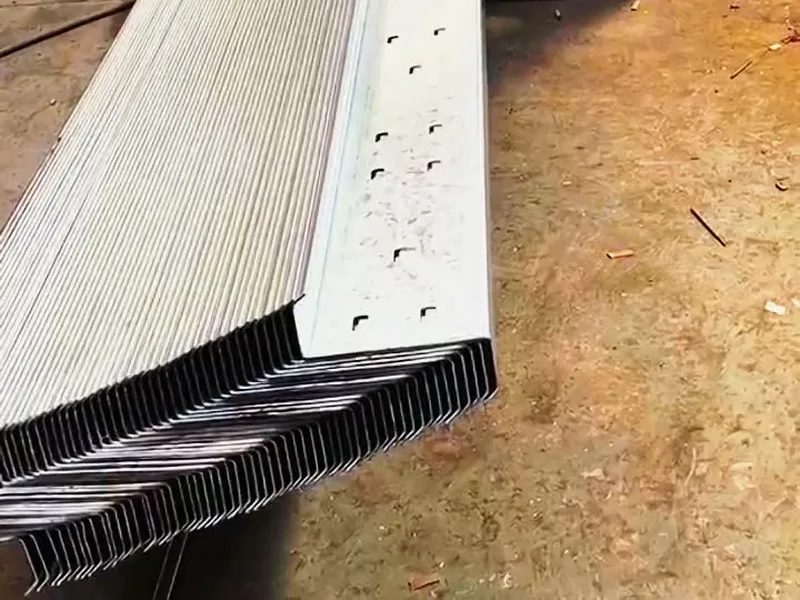
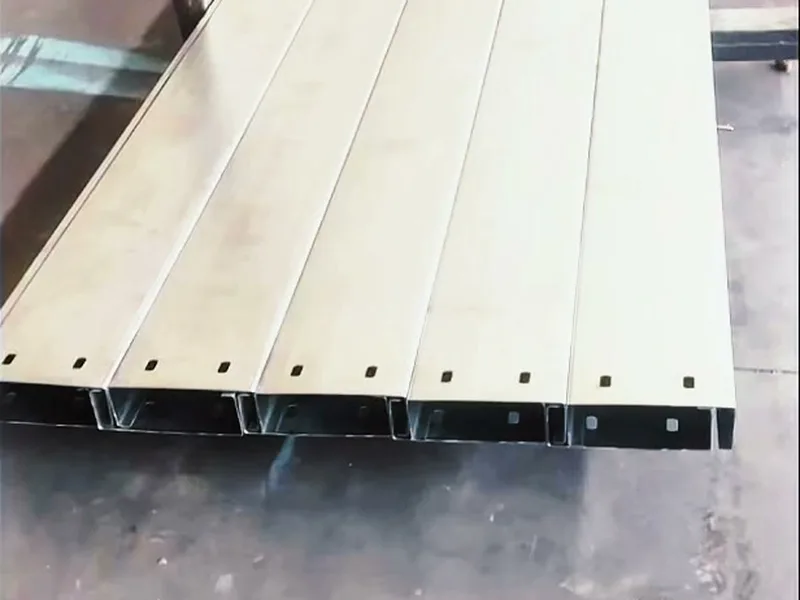
our Xiamen production base's public HCZ-S20 listing shows a C-section drawing, a Z-section drawing and a photograph of formed sections. They help identify the shapes and the dimensions to send for quotation; they are not measured acceptance samples for a Halcyon order.
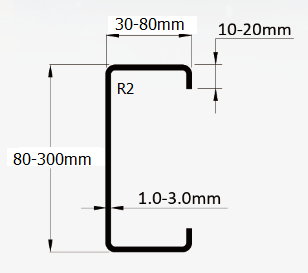
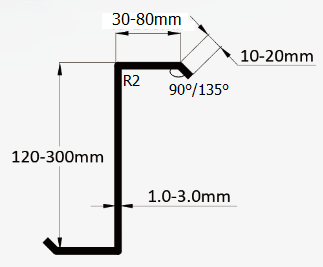
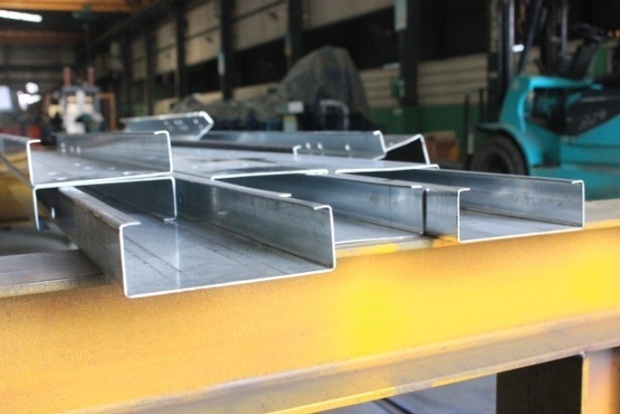
Document difference to resolve: the separate model-family comparison used in the table above lists HCZ-S20-300 C/U from 75 mm, while the public HCZ-S20 C drawing begins at 80 mm. These are different references. Ask the named factory to confirm the current quoted model, minimum C size, included tooling and both C and Z trial pieces in writing. HCZ-S20 source page.
Ask for the station layout of the named configuration. Pre-cutting separates the strip before roll forming; post-cutting cuts the formed section. The alternatives below explain the sequence, not two standard modes guaranteed on every machine.
Confirm the actual punching position, any marking station, stop-to-cut or flying-cut method, and the transfer of cut pieces in the proposed layout. The quotation states which route is included and whether both are available on the same build.
Use the same C and Z drawings, coil specification, hole schedule and finished lengths for the trial. Check finished length, end shape, burrs, hole position relative to the agreed datum and the profile dimensions on first-off and repeated pieces. Include stops, scrap and discharge handling when recording accepted output. Resolve the tooling and cut-off setup after each required size or C/Z change.
Use the cut-off station inspection checklist and the C/Z changeover trial record with our written proposal. No route-specific speed, minimum cut length or universal tool compatibility is asserted.
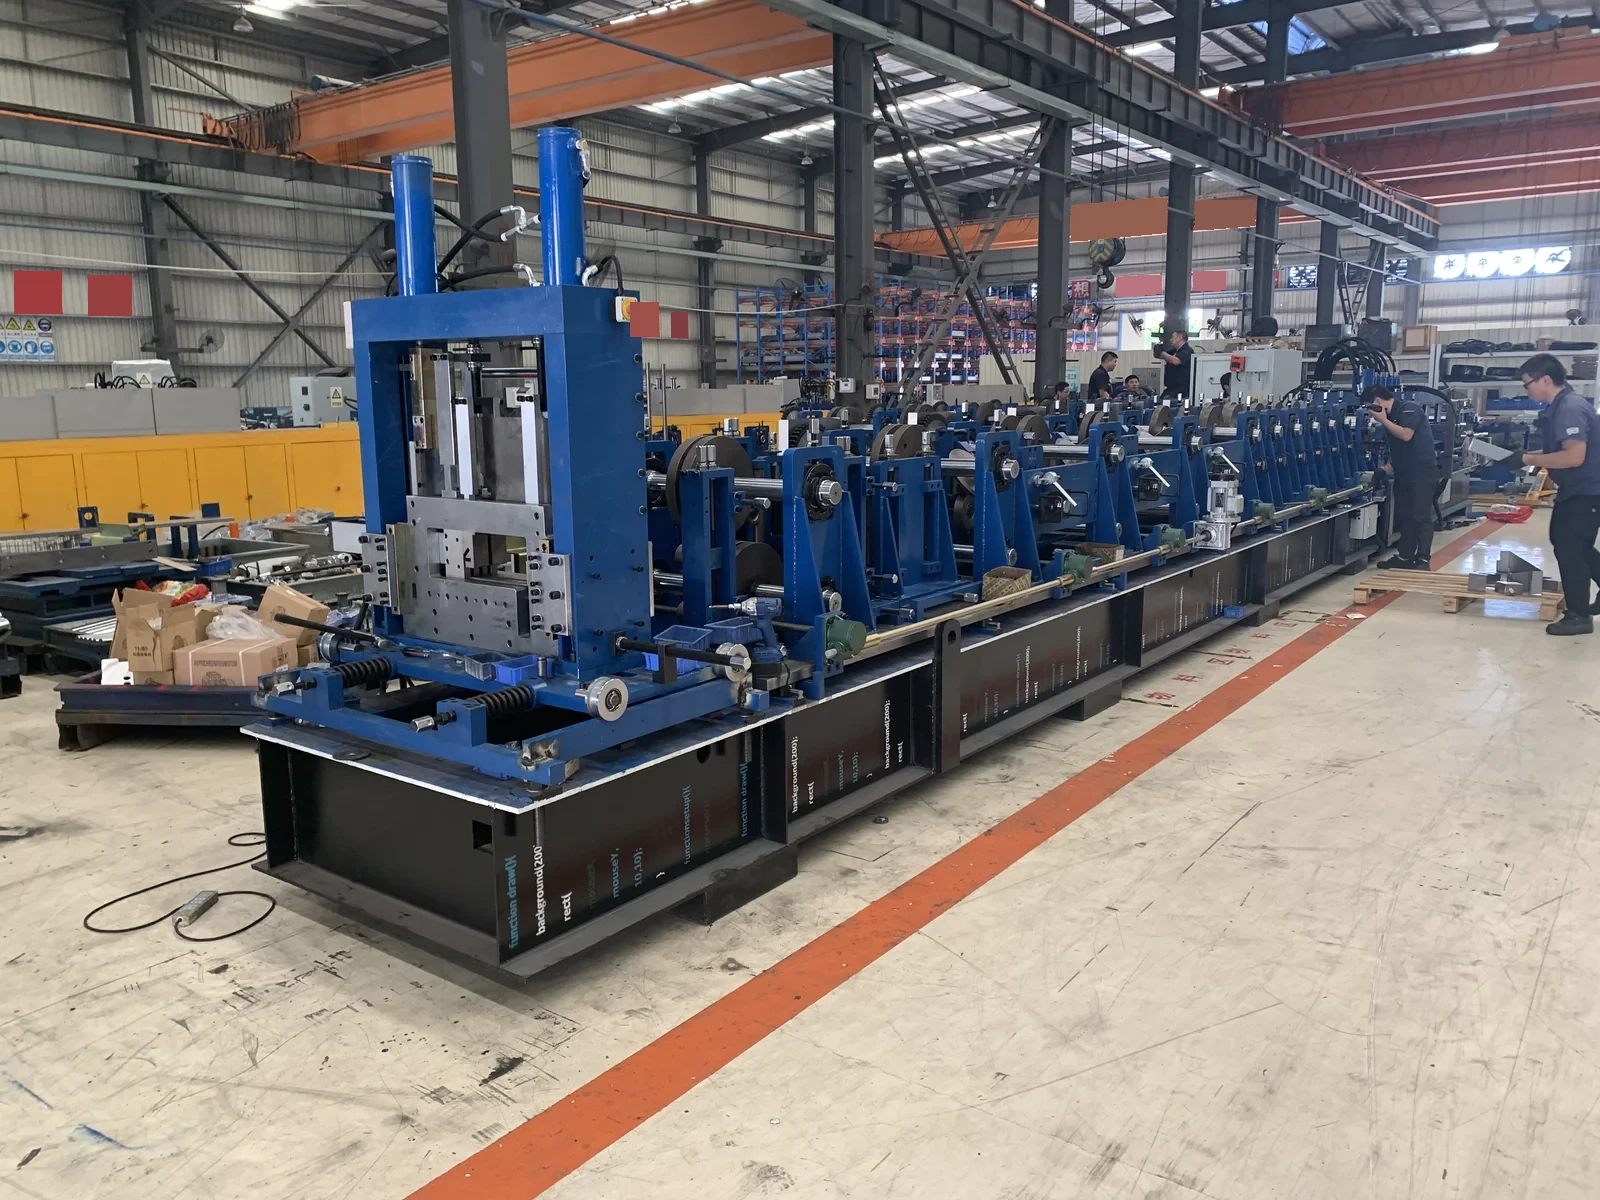
These two distinct workshop photographs show forming stands and a line layout. They do not show a completed production trial, identify the quoted configuration, or prove output or acceptance results.
Options are quoted only when they match the approved production workflow.
Manual, hydraulic or powered decoiler selected for the specified coil weight.
Servo or hydraulic punching and marking arranged to the approved hole schedule.
Manual, motorized or recipe-driven adjustment according to the product family.
Pre-cut, post-cut or flying cut selected for profile stability and cycle time.
Run-out table, stacker, bundling or robot transfer for the required output.
Destination voltage, component brand, guarding and documentation language.
Flexible C and Z purlin production for industrial buildings, warehouses and structural steel projects. If your approved production list contains only C or only Z sections, compare the dedicated line against an automatic C/Z changeover proposal before selecting tooling.
No. Changing the dimensions of a C section and changing between C and Z shapes are separate tasks. A recipe screen or servo-adjustment clip cannot establish that the quoted line performs both without manual tooling work. Ask our factory team to list each required movement, adjustment and tool change for your C and Z drawings.
| Task | What the trial must identify | Buyer record |
|---|---|---|
| Change size within one shape | Initial and target drawings, recipe, roll and guide adjustment, punching and cut-off setup | Record manual work, setup time and measured first-off parts for both sizes. |
| Change C to Z, then Z to C | Shape conversion, tooling orientation, required replacements and operator steps in each direction | Time each direction separately and identify the measured C and Z samples. |
| Restart accepted production | Specified steel and thickness, holes, cut length and downstream handling | Record the first conforming part and rejected pieces; agree the start and end points before timing. |
For a quoted changeover time, specify whether it ends at the last setup movement or at the first measured part that meets the agreed drawing. Use the C/Z changeover test record with the written configuration. No changeover time or fully automatic operation is promised for an unselected build.
the published model listing described five named families, and the final specification for your order is set from your own drawings. Start with the required C and Z drawings, steel grade, thickness range, punching layout and target output. Compare the included tooling and a witnessed size or shape change before choosing a quoted build.
| Published family | Listing scope | Buyer check before quotation |
|---|---|---|
| N Series | HC-300N C only · HZ-350N Z only · HCZ-300N C/Z | For C/Z production, confirm HCZ-300N and witness both directions. |
| S Series | HC-300S C only · HCZ-300S C/Z | For C/Z production, confirm HCZ-300S and its supplied tooling. |
| F Series | HC-300F C only · HCZ-300F C/Z | Confirm HCZ-300F for C/Z and the supplied tooling. |
| L Series | HC-300L C only · HCZ-300L C/Z | Confirm LS versus LN before assuming Z capability. |
| M Series | M Series C only | Confirm the exact C profile, punching and cut-off scope. |
Source: These model codes and profile types come from the published model listing; current availability, speed, thickness and tooling are confirmed in the factory quotation and a witnessed trial.
Send a dimensioned cross-section plus hole locations, finished lengths and any critical tolerances.
No. Guaranteed output depends on steel grade, thickness, profile, punching frequency, cut length and handling method.
The proposal lists the line modules, layout, electrical standard, exclusions, test material, delivery scope and production assumptions.
Before handover, agree controller and operator-panel backups, software versions, licence terms and maintenance access. Use the PLC backup and control-system handover guide to distinguish restoration files from an editable project. Rights to edit the control program are agreed separately from the production-order import function.
Use our roll forming machine quotation checklist to send the drawing, material, operations and acceptance details an engineer needs.
A forming trial also depends on how the specified coil is loaded and fed. Record coil identification, inner diameter, loading method, strip direction and the first feed check alongside the approved C and Z drawings. Use the coil loading trial record to prepare those observations; it does not replace a measured profile or punching acceptance test.
A workshop video can show the forming section and material path. It cannot, by itself, verify the buyer's approved profile dimensions, a complete C-to-Z changeover, production output or acceptance tolerance.
Give the supplier the revision-controlled profile drawing, steel grade, thickness range, punching layout and target output. For each C and Z profile, request an identified trial sample, measurement record, setup or changeover record and any unresolved deviations. Compare those records with the agreed acceptance method; do not infer a guarantee from this clip.
For the general method, see our FAT evidence checklist. To discuss your own parts, leave an email for technical follow-up.
Direct answer: We quote every automatic C/Z purlin machine by configuration, not from a fixed price list. The price depends on the profile drawing, material thickness, punching and cutting, the level of automation and the delivery terms. Send your drawing and we reply with a written quotation for that exact configuration.
| Configuration level | What changes | Usually chosen for |
|---|---|---|
| Basic fixed-size C or Z line | One section size per tooling setup; sizes changed manually by adjusting or replacing tooling. | Steady orders for one or a few standard sizes |
| Quick-change C/Z line | C and Z sections from one line, with faster shape and size changeover. | Mixed C and Z orders with regular size changes |
| Fully automatic stepless C/Z line | Section width and height set from the control system within the line's size range, with automatic punching and cut-off. | High-mix production and frequent size changes |
Price rises from the first level to the third as tooling, servo control and automation are added.
Roll forming machines from Halcyon's Xiamen factory have been used on 150+ construction projects (2022–2026) in China and abroad, including an airport in Iraq, a national stadium in Senegal, resort buildings in the Maldives and a coal preparation plant in Mongolia. See the reference projects.
Direct answer: An automatic C/Z purlin machine price is meaningful only with a defined set of C and Z drawings, coil grades and thicknesses, hole layouts, finished lengths and accepted output target. A headline price cannot tell a buyer whether punching tools, the decoiler, discharge equipment, guarding, commissioning or an acceptance trial are included.
| Quotation input | What to specify | What to compare in the offer |
|---|---|---|
| Finished C and Z sections | Revision-controlled drawings, flange/lip details and required size list | Which sections and C-to-Z transitions the proposed tooling actually covers |
| Coil and output | Steel grade, thickness range, coil dimensions, cut lengths and accepted pieces per shift | Test material, line-speed assumption and downstream handling included in the output claim |
| Punching layout | Hole type, diameter, datum, spacing and location on each section | Punches, dies, control recipe and identified samples for both C and Z parts |
| Delivery and acceptance | Destination electrical standard, layout and trial method | Decoiler, run-out, stacker, guarding, documents, service, exclusions and acceptance evidence |
Ask suppliers to quote the same drawings and acceptance method. Compare the signed scope and measured trial results before comparing prices. For the wider purchase budget, use the roll forming machine cost guide and editable worksheet to separate equipment, freight, site startup and first-year operation. Halcyon works directly with the factory production team on that review; this page does not state a price, lead time or guaranteed performance for an unselected line.
Source and scope: Halcyon Machinery procurement review, updated 26 September 2026. The comparison is guidance for preparing a request, not a claim that all listed modules are standard on every model. See the C/Z changeover test record and quotation checklist.
A profile drawing and a machine-ready order file are different deliverables. The drawing defines the section and inspection criteria. An order file may identify parts, quantities, lengths and hole operations, so confirm compatibility with the quoted controller in writing. Automatic shape changeover and a CAD-to-machine interface are separate items to specify.
Ask us to identify the design or scheduling software and version, the exported format and revision, and the proposed machine controller and software version. State whether the job is imported directly, converted by a specified tool or entered manually. Agree conversion or licence costs, the handover files and responsibility for later software changes. Halcyon does not claim universal CSV, DXF or any named CAD-package compatibility for an unselected C/Z line.
| Check | Record before acceptance |
|---|---|
| Source revision and units | Retain the approved drawing and job revision, part IDs, units, C/Z orientation and cut lengths used in the trial. |
| Operation mapping | Compare each hole or slot position, datum and tool code with the proposed tool set. Record rejected rows, warnings and omitted operations; do not silently treat them as accepted. |
| Finished-part verification | Run the agreed job on the proposed configuration. Identify each trial piece and check dimensions, holes and any quoted part marking against the approved drawing. |
| Revision and restart | Repeat the agreed checks after a controlled job revision or restart. Record which file produced each piece and any manual intervention. |
Download the blank C/Z order-file review record. It is a buyer worksheet, not a machine input file, accepted controller format or completed trial report.
Why ask: CAD order transfer and individual part identification are common buyer requirements on automatic C/Z lines, so confirm early how the line receives orders and marks each part. For a separate LGS framing order, use the framing-machine job-file guide; its model examples do not prove C/Z compatibility.
Send one non-confidential example order with the profile and punching drawings through the quotation enquiry. We will review the requested interface and obtain a configuration-specific import and trial plan before including it in the proposal.
We will confirm the suitable model, process route, line modules and the values that can be guaranteed for your material.
New buyer guide: How to review a finished profile sample.
For a quoted automatic C/Z configuration, record both C-to-Z and Z-to-C setup steps and measured first-off samples. Use the buyer changeover test record alongside the approved drawings and the written proposal for your line.
If a first-off profile misses an angle on the approved drawing, the flange-angle trial review shows how to record measured samples and tooling adjustments before acceptance; it does not set a universal tolerance.
Check guarding for the quoted C/Z line before accepting a line layout or trial. The written quotation, not the photo, defines the safety scope.
Use the blank Z-purlin lap and hole-alignment trial record to identify both pieces, the connection drawing, orientation, hole datums, actual measurements and trial-fit observations. Repeat the record after a relevant size or recipe change. Record unresolved results and the agreed repeat test; do not turn an unmeasured visual fit into a pass.
Read the paired-part Z-purlin lap acceptance guide for the trial sequence and the boundary between machine acceptance and structural approval.
This blank worksheet records observations. The project engineer supplies the connection design and acceptance limits; it does not establish structural capacity, approve installation or replace agreed machine acceptance documents.