
Z Purlin Roll Forming Machine
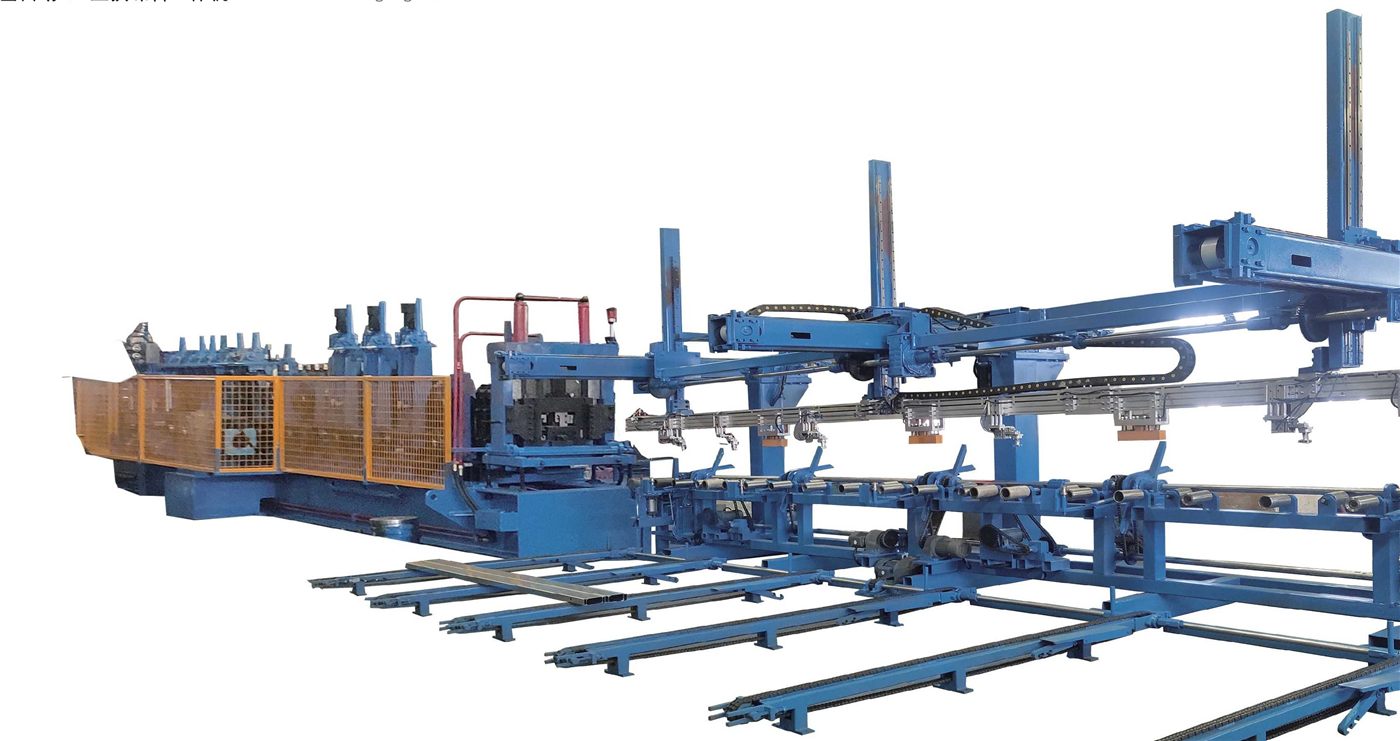
Factory-direct Z purlin lines built at our Xiamen manufacturing base and configured to your Z-section drawing, lap length and bolt-hole pattern — as a dedicated Z machine or a combined C/Z line.
Price range: C/Z purlin roll forming machines
US$39,000–62,000 (standard) · US$72,000–143,000 (premium), FOB China
Standard covers the first two configuration levels (single-profile and multi-profile / quick-change); premium covers fully automatic lines.
Final price depends on profile, thickness, speed, punching and automation. Excludes freight, import duties and installation. Send your profile drawing for a quotation within 24 hours. North American configurations (480V/60Hz, UL and local requirements) are quoted separately.
Large complete lines (e.g. truck chassis beam lines or full cable tray lines) are quoted per project, typically above US$150,000.
Manufactured in our Xiamen factory · 35+ years of roll forming experience.
Get a quote for this machine
Send your profile drawing or a photo of the profile. We reply within 24 hours with a configuration and price.
Commercial terms
- Lead time
- standard machines 30–60 days; automatic and heavy-duty lines 60–120 days (confirmed in the quotation).
- Warranty
- 12 months on the machine, lifetime technical support by video and remote guidance; wear parts excluded.
- Payment
- 30% deposit; 70% before shipment, after you approve the trial-run video.
- Shipping
- FOB Xiamen, China.
How should a Z purlin line be specified?
Direct answer: Start with the approved Z-section drawing and the engineer's lap and bolt-hole details. A Z profile can be used in lapped purlin arrangements, but the required lap length, hole locations and structural capacity are project-specific. The machine trial should prove that the proposed tooling makes the specified section and repeatable holes.
- Drawing inputweb, flange, lip, thickness range, grade and dimensional tolerances
- Joint inputapproved lap length, handedness, hole pattern and reference datum
- Production inputcut lengths, size mix, changeover sequence and target output
- Trial evidencefirst-off and repeat section dimensions, paired lap fit, hole registration and cut-end quality
What should the sample trial record?
Agree the drawing revision, measurement datums and trial material before the test. A single attractive section is insufficient: compare the first accepted part with later parts and a paired lap assembly. Keep the machine setting and measured results with the sample IDs so a later buyer review can distinguish a tooling adjustment from stable production.
| Buyer question | Trial input | Acceptance evidence |
|---|---|---|
| Will the specified Z section form? | Approved web, flange and lip drawing; steel grade and thickness range. | Measure first-off and repeat dimensions on identified pieces against agreed tolerances. |
| Will the lap assemble? | Engineer-approved lap detail, orientation and handedness. | Fit two sampled parts together and record overlap and joint fit; do not infer structural capacity from fit alone. |
| Will holes register after forming? | Hole schedule and a clearly defined datum on the profile and lap. | Measure paired-hole locations on the assembled samples, including the first and later pieces. |
| Can the required mix be produced? | Order lengths, size changes, target output and intended cut/punch sequence. | Witness the requested recipe or tooling change, count good parts and record setup scrap and cut-end condition. |
Machine capability for your Z sizes is confirmed in the signed technical agreement; structural lap design remains with your project engineer.
When is a combined C/Z line appropriate?
A combined line may be proposed if both C and Z drawings are within its verified tooling envelope. Ask for a witnessed C-to-Z and Z-to-C changeover using the required sizes and hole layouts. Whether changeover is automatic or manual, and how long it takes, is confirmed in the quotation for your sizes. See the configured C/Z machine page and the C versus Z selection guide.
Send us your profile drawing
We will review your profile drawing, material, hole pattern and target output with our factory engineers in Xiamen, then confirm the proposed machine scope and quotation.
Get a quoteHow much does a Z purlin roll forming machine cost?
Direct answer: We quote every Z purlin roll forming machine by configuration, not from a fixed price list. The price depends on the profile drawing, material thickness, punching and cutting, the level of automation and the delivery terms. Send your drawing and we reply with a written quotation for that exact configuration.
| Configuration level | What changes | Usually chosen for |
|---|---|---|
| Basic fixed-size C or Z line | One section size per tooling setup; sizes changed manually by adjusting or replacing tooling. | Steady orders for one or a few standard sizes |
| Quick-change C/Z line | C and Z sections from one line, with faster shape and size changeover. | Mixed C and Z orders with regular size changes |
| Fully automatic stepless C/Z line | Section width and height set from the control system within the line's size range, with automatic punching and cut-off. | High-mix production and frequent size changes |
Price rises from the first level to the third as tooling, servo control and automation are added.
What affects the price
- Z section size range and lap (overlap) requirements
- Steel thickness and yield strength
- Dedicated Z line or combined C/Z line
- Punching layout and cut-off method
- Manual, quick-change or fully automatic size change
- Control system and main component brands (PLC, servo, hydraulics)
- Decoiler, outfeed table and automatic stacking
- Delivery terms (FOB or CIF), packing and spare parts
Roll forming machines from Halcyon's Xiamen factory have been used on 150+ construction projects (2022–2026) in China and abroad, including an airport in Iraq, a national stadium in Senegal, resort buildings in the Maldives and a coal preparation plant in Mongolia. See the reference projects.
Compare a dedicated Z line with a combined C/Z line
A dedicated Z line may be appropriate when the order mix is consistently one Z family; a combined line is worth reviewing when the buyer also needs approved C sections. Compare quoted tooling and changeover steps against the same drawings, steel grades, lap-hole patterns, cut lengths and target accepted output. Our quotation lists any profiles that need a separate setup or fall outside the quoted line.
Does paired lap fit prove the Z purlin's structural capacity?
No. It shows the sampled geometry and hole registration. The project's responsible engineer must assess loads, restraints, overlap and connections.
What makes a changeover demonstration useful?
Start from the last accepted C part, record operator actions and rejected setup pieces, then measure the first accepted Z part. Repeat Z-to-C with the buyer's required holes and lengths.
What should both suppliers quote on the same basis?
Use the same approved C and Z drawings, material ranges, punching layouts, production mix, target output and acceptance method. Request a written inclusion list for tooling, handling and controls.
What does a published C/Z machine tell you about Z production?
HCZ-350F product sheet is a published production-base example of a combined line. It describes gearbox drive, leveling, pre-punching, pre-cutting, a roll former, hydraulic cutting and product support. It is a C/Z model reference; a dedicated Z line may be arranged differently.
| Published HCZ-350F information | Confirm for your Z-section order |
|---|---|
| Punching on flat strip, with some positioning adjusted manually | Hole datums, adjustment actions, supplied punches and paired-lap registration after forming |
| Size adjustment and C/Z interchange are described separately | Which actions are automatic, which require an operator, and the first accepted Z part after each change |
| The quick details list 35 m/min; the main roll-former section lists 0–30 m/min | A signed speed definition and the tested configuration; the two published figures need clarification |
| The machine stops for punching and cutting | Accepted pieces per timed batch with your hole pattern, lengths and size changes included |
For a comparable proposal, send the same drawing revision, lap detail, steel and thickness range, length schedule and batch mix. Ask for the offered station layout, current machine identification and recorded measurements. A supplier's catalogue figures support a technical discussion; use the agreed trial to establish your actual configuration and accepted output.
Review the automatic C/Z equipment scope and the changeover test record alongside the paired Z-lap trial below.
Record the paired Z-purlin lap trial
Use the blank Z-purlin lap and hole-alignment trial record to identify both pieces, the connection drawing, orientation, hole datums, actual measurements and trial-fit observations. Repeat the record after a relevant size or recipe change. Record any unresolved result together with the agreed repeat test.
Read the paired-part Z-purlin lap acceptance guide for the trial sequence and the boundary between machine acceptance and structural approval.
The project engineer supplies the connection design and acceptance limits.