
HSP-200 Multi-Size Secondary Purlin Line: Changeover Trial
Our Xiamen production base lists HSP-200 as a multi-specification secondary-purlin former. Its public listing does not establish the exact size range, changeover method or finished-part output for your order. Test the requested sections and return to the first size before accepting a proposed configuration.
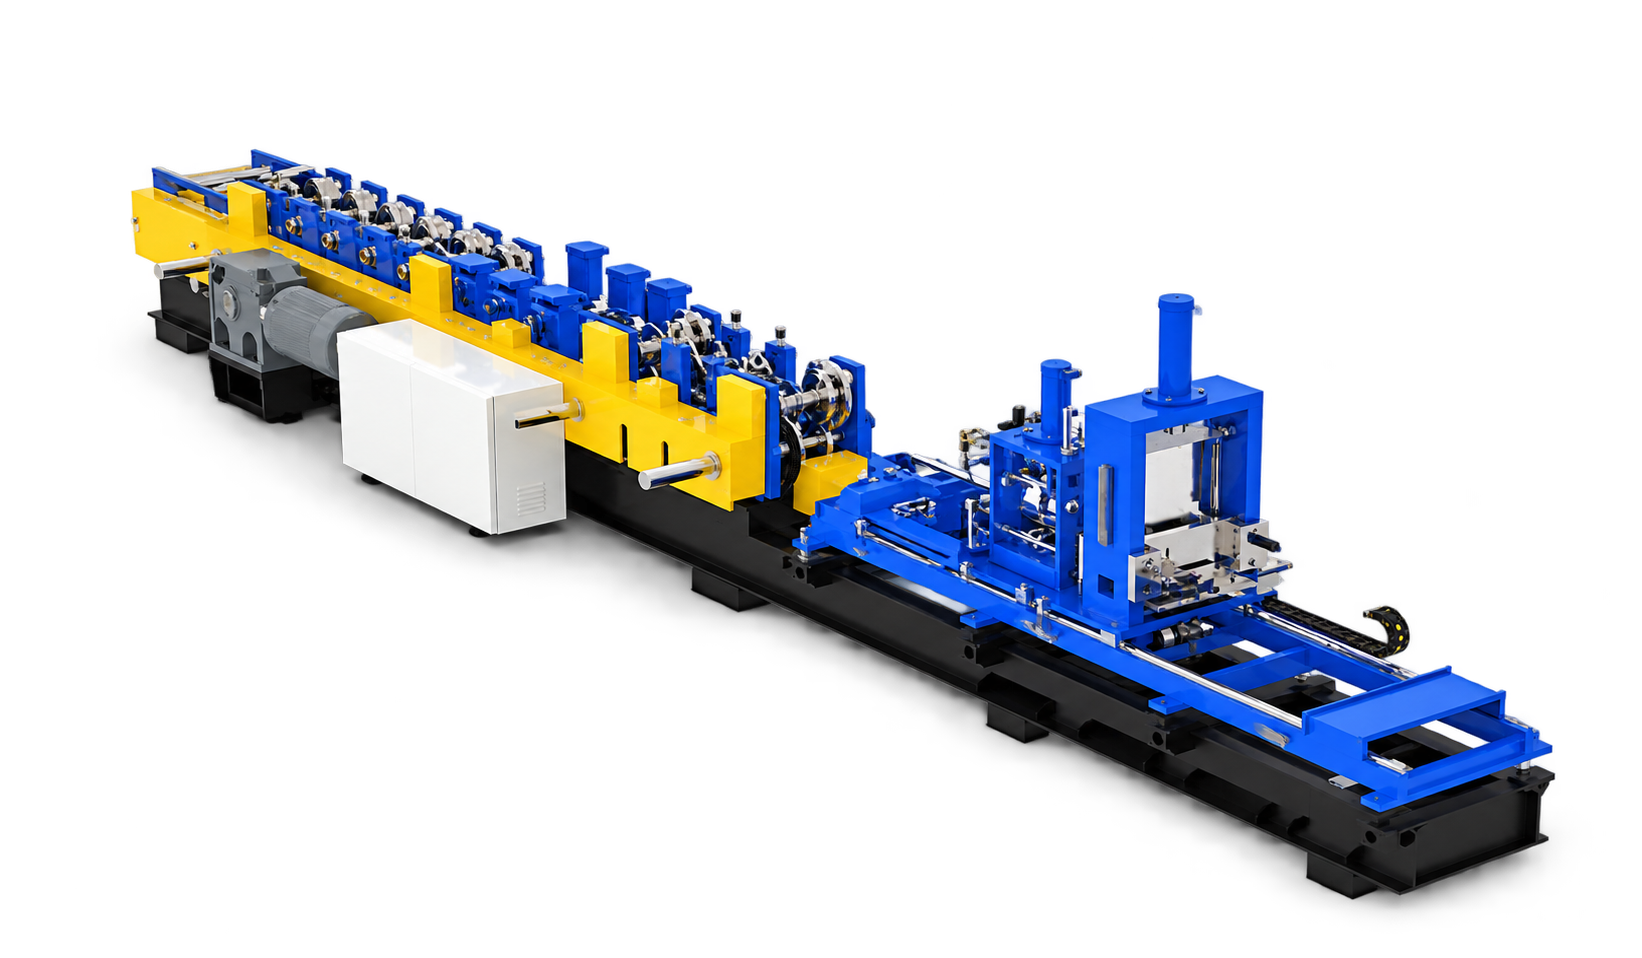
Production-base rendering. Confirm the current build and offered modules with dated evidence.
What proves one HSP-200 line suits several purlins?
A model name is not enough: the proposed tooling and trial must cover every ordered section. Supply drawings for the smallest, largest and most frequent secondary purlins, including return lips, hole schedules, cut lengths and material grades. Ask our factory team to show which rolls, guides, punches, cutters and controls change between them. A programme selection is not proof that mechanical tooling moves automatically.
If one section needs separate roll sets or a different cut-off, price that scope explicitly. Compare HSP-200 with the documented automatic C/Z configurations only after both proposals use the same finished-part schedule and trial conditions.
Separate the published model name from the quoted machine
Our Xiamen production base's HSP-200 listing identifies a multi-specification secondary-purlin former, but its public text does not provide an order-ready technical standard. The table below is a quotation checklist, not a specification claim.
- Profile envelope
- Supplier to name the exact approved sections and tooling range
- Size adjustment
- Supplier to show manual, powered or programmed actions for each axis
- Punching
- Match each hole layout, die and datum to its section
- Cut-off
- Identify blade/tool changes and end condition for each profile
- Controls and records
- Show recipe fields, interlocks and saved setup values in the offered design
- Useful output
- Measure with the agreed batch, material, holes and handling sequence
No speed, thickness, accuracy or changeover time is represented as an HSP-200 guarantee here. Put verified acceptance values in the signed technical agreement.
Run an A–B–A changeover trial
Start with one agreed purlin size and preserve first-off and later pieces. Change to a second drawing, recording every manual adjustment, tool exchange, die change, controller step and elapsed setup time. Return to the first drawing and measure it again. This exposes repeatability and hidden changeover work that a single demonstration run can miss. Compare web, flange, lip, hole datum, cut length and fit using the same defined measurement method.
Reference rendering and real build evidence
Questions that affect the purchase decision
Does “multi-size” mean tool-free automatic changeover?
No. The public model name does not state which adjustments are automatic. Ask for a station-by-station changeover list and witness the A–B–A trial.
Can HSP-200 make my C and Z sections as well?
Do not infer that from “secondary purlin”. Submit each approved profile drawing and compare tooling and trial evidence with a dedicated C/Z proposal.
What evidence should be attached to the offer?
The exact line layout and module list, supported drawings, material and hole schedule, changeover actions, trial criteria, samples and exclusions.
Source and limits: HSP-200 product listing, checked 24 September 2026; Halcyon Machinery buyer-review method, updated 24 September 2026. The listing establishes the model family but no independently checked production range or customer case.
Send the full secondary-purlin schedule
We will ask our factory team to map each section to a configuration and documented changeover trial.
- Smallest, largest and frequent section drawings
- Grade, coating and thickness range
- Hole layout and cut-length schedule
- Batch mix and target output
- Required trial and acceptance method