
U-section matrix
List every target width, height and return dimension. Request written tooling coverage for the agreed steel and thickness at each size.
A multi-size U-section line for solar mounting components. Match your rail drawing and punch schedule to the offered HSU-150 before comparing output claims.
Our Xiamen production base describes a single-U reference family with 70–150 mm published web width, 30–70 mm section height and 2.0–3.5 mm material thickness. These are catalogue limits for a family, not proof that every width, height, steel grade and hole pattern can be combined in one quoted build. Supply the approved section, steel grade, thickness range, punching layout and target output for review.
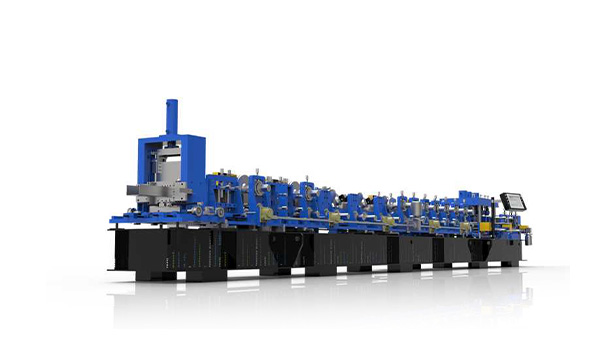
Our Xiamen production base's catalogue visualization, not a photograph of the offered build. Confirm the current machine and trial parts before purchase.
This page addresses a multi-size U-channel decision, distinct from HSM-41's compact 41.3 mm-base strut channel.
List every target width, height and return dimension. Request written tooling coverage for the agreed steel and thickness at each size.
Ask the supplier to demonstrate a size change using the offered controls and record the settings and first acceptable part.
Use a revision-controlled hole and slot layout. Measure centres, edge distances and repeat pitch on identified samples after a size change.
Record coil grade, thickness, part length and hole density during the run. A catalogue speed is not an order-specific shift output.
Values below separate confirmed product information from project-dependent engineering data.
Source and boundary: family dimensions, thickness, control route and reference speed are from our Xiamen production base's SU-series product description, checked 26 September 2026. Its speed and accuracy figures are published references, not verified results for your material or hole density. The signed technical agreement and measured trial govern the final values. Reviewed by Halcyon Machinery on 26 September 2026.
Agree the test coil, two drawings and acceptance points before the run.
We provide the current machine layout, component list, sample profile and test plan for the exact quotation.
Separate the published model family from the equipment and tooling in a specific order.
Give every U-section size, flange return and tolerance in a drawing matrix. Mark mandatory and optional sizes.
Confirm steel grade, yield range, coating, thickness and coil dimensions for each section.
Identify slots, round holes, pitch and edge distances; request a sample from the offered die set.
Our Xiamen production base describes industrial-PC control and USB or network import. Confirm file format, revision handling and changeover records.
Measure section and hole location at two selected sizes, with coil identity and trial time recorded.
List coil handling, cut-off, run-out, guarding, electrical standard and commissioning responsibility.
Choose HSU-150 only after confirming the multi-size U-section range. A compact strut-channel drawing may point to HSM-41 or another tool set.
No such capability should be inferred from the HSU-150 name. Ask for the exact ordered tooling, supported drawings and separate C/Z trial evidence if needed.
Record the starting and target U drawings, settings, elapsed changeover and the measured first acceptable part at both sizes.
No. Output depends on coil, slot density, part length, cut-off and handling. Agree a trial or cycle calculation for the actual order.
We will confirm the suitable model, process route, line modules and the values that can be guaranteed for your material.
Hole pitch, transverse location and cut-end offsets answer different acceptance questions. Use the U-channel size-change hole-datum guide to connect each drawing to identified first-off and later samples.