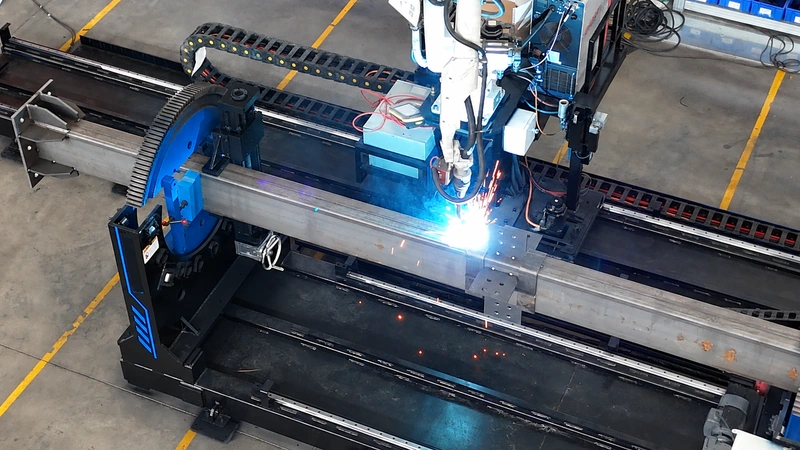
Buyer answer: The cell should be evaluated against a real representative part, an approved weld map and measurable weld acceptance criteria. Robot reach, positioner layout and throughput are consequences of that workpiece and the proposed process, not reliable figures to borrow from a generic catalogue.
Factory photo of an HWR-1240F robotic welding workstation, from our Xiamen production base's model reference. This shows the welding process; it is not evidence of the proposed configuration, weld acceptance or output for your part.
Halcyon handles equipment enquiries factory-direct from our Xiamen production base. The model and configuration are not verified by a branded illustration, and this page does not claim an in-house robot cell, measured productivity gain or completed customer acceptance test.
Robot arm, standard cell or a custom structural welding station?
A robotic welding cell is a complete production arrangement. Match the workpiece, loading route and weld access before deciding which arrangement to quote. These are purchasing alternatives to review, not a promise that every package is available from Halcyon.
Robot and welding package
Suitable for comparison when you already have an integration plan. Identify who supplies the fixture, positioner, guarding, extraction, utilities, controls and acceptance trial. An arm and power source alone do not establish a usable production cell.
Pre-engineered cell
Check the documented workpiece envelope, loading access and positioner arrangement against your actual part. Standard equipment still needs the correct fixtures, programs, weld procedure and inspection. Do not infer that a compact-cell layout will handle a long beam or obstructed node.
Part-specific structural station
Use a drawing-led layout review when long members, attachments or intersecting connections need their own support and seam-access strategy. Separate handling time from welding and inspection, and trial the hardest representative joint.
Choose the structural workpiece route
For long members and attachments, review the HWS-1260 structural-member welding station and check support, turning and joint access. For intersecting members and connection assemblies, review the HWS-500 structural-node welding workstation and check fixture datum, node variants and access around each seam. Neither model name establishes capacity or weld acceptance for your part.
Industry terminology reference: OTC DAIHEN's published cell arrangements illustrate how part handling and positioning differ among cell types. This reference does not describe a Halcyon configuration, brand partnership or guaranteed result.
Does the welding-cell load include the fixture?
For a positioner, ask for approval of the workpiece and fixture together. A part weight alone does not establish whether the quoted arrangement can hold and turn it. Identify the complete loaded assembly and ask our factory team to approve its dimensions, mounting and operating positions.
Workpiece: provide the assembly drawing, mass, joint locations and part variants.
Fixture: include clamps, locating devices and other equipment carried by the positioner; record the complete loaded mass.
Rotation and access: submit the loaded envelope and mounting drawing. Ask which orientations, movement conditions and robot access are included in the approved layout.
Robot tooling: request a separate check of the torch, mounted equipment and required reach. A robot specification does not replace approval of the workpiece-positioning arrangement.
Download the blank workpiece and fixture review and attach it to the assembly drawing. It collects requirements and supplier responses; it is not a capacity certificate or a completed test.
Technical reference: ABB's IRP B positioner description explicitly includes the fixture with the workpiece in its handling capacity. This establishes a comparison question only; ABB ratings are not adopted as Halcyon or HWR-1240F specifications. Reviewed 3 October 2026.
Inputs for our factory team
Part and fixtureDimensioned assembly drawing, part mass, datum points, incoming fit-up and clamping constraints.
Weld definitionWeld map, joint access, material grade, thickness range, welding procedure and required inspection standard.
Production mixRepresentative part family, batch size, shift pattern and target finished output.
Site requirementsAvailable power, floor space, extraction, shielding-gas arrangements and destination safety requirements.
Evidence to agree before an order
Ask for a fixture concept and a reach study against the actual assembly. Define how the sample weld will be inspected, who signs off defects and which part variations will be demonstrated. A trial record should distinguish arc-on time, loading/unloading and rework; quoting only robot travel or arc speed does not establish finished-part output. Safety guarding, operator access and extraction must be reviewed for the destination plant.
This is a fabrication and welding selection problem. A roll forming line uses different tooling and acceptance criteria; do not infer robot suitability from a profile machine photo.
Send us your requirement
Send the assembly drawing, weld map and representative part family. We will identify what our factory team needs to verify before proposing a cell.
Our factory team should confirm reach, welding process, fixture, positioner, guarding and inspection with the workpiece and weld procedure. No reach, payload, cycle-time or payback figure is promised on this page.
Provide the assembly drawing, steel grade and thickness, weld map, target output, current fit-up method, available utilities and destination country.
Does robot welding automatically remove rework?
No. Part fit-up, fixture repeatability, welding procedure and inspection determine the actual result. Require a witnessed sample and rejection record for your own part.
Can you estimate a payback now?
Not from this page. A comparison needs verified cycle time, loading, consumables, rework and labour assumptions for the proposed cell and current process.
Welding robot price: compare the complete cell scope
Buyer answer: A robot-arm price and an installed robotic welding cell quotation cover different equipment and responsibilities. Send the same representative steel assembly, weld map, material, fit-up variation and inspection criteria to each bidder. Compare the proposed scope line by line before comparing totals; Halcyon does not publish a verified fixed price or lead time for your cell on this page.
Items to confirm in a steel-fabrication welding cell proposal
Quotation item
Evidence and responsibility to agree
Robot and welding equipment
Identify the proposed robot, controller and welding equipment. Confirm the process against the actual joint; a generic robot name does not establish process suitability.
Fixture and part positioning
State which fixtures, positioners and any travel axis are included. Review reach, access and allowed part variation with the assembly drawing and trial workpiece.
Cell integration and plant interface
List guarding, interlocks, extraction interface, loading arrangements and utilities. Identify the provider and site responsibilities; a proposal is not proof of destination compliance.
Software and program delivery
Identify the controller and software versions, licences, part and fixture model revisions, and the program files or backups included in handover. If offline programming is quoted, confirm the supported input and postprocessor for that exact cell. Agree who checks the transferred program against the real fixture, robot setup and inspected trial welds; a simulation alone is not a completed weld acceptance test.
Trial and handover
Agree the representative parts, weld inspection, accepted-part output record, corrective work, documentation and training included in acceptance.
Delivery and continuing service
Separate packing, shipping terms, installation, commissioning, consumables, spares and service exclusions. Obtain written commercial terms for the destination plant.
Record loading, welding, unloading, inspection and rework when comparing trials. Keep the same part and acceptance criteria; a faster robot movement alone does not prove lower cost per accepted assembly. Send the assembly drawing and request an itemised cell proposal.
Review updated 3 October 2026. This is a purchasing checklist, not a completed test, a price list or a promise that every listed module is supplied.